
QUICK ANSWER
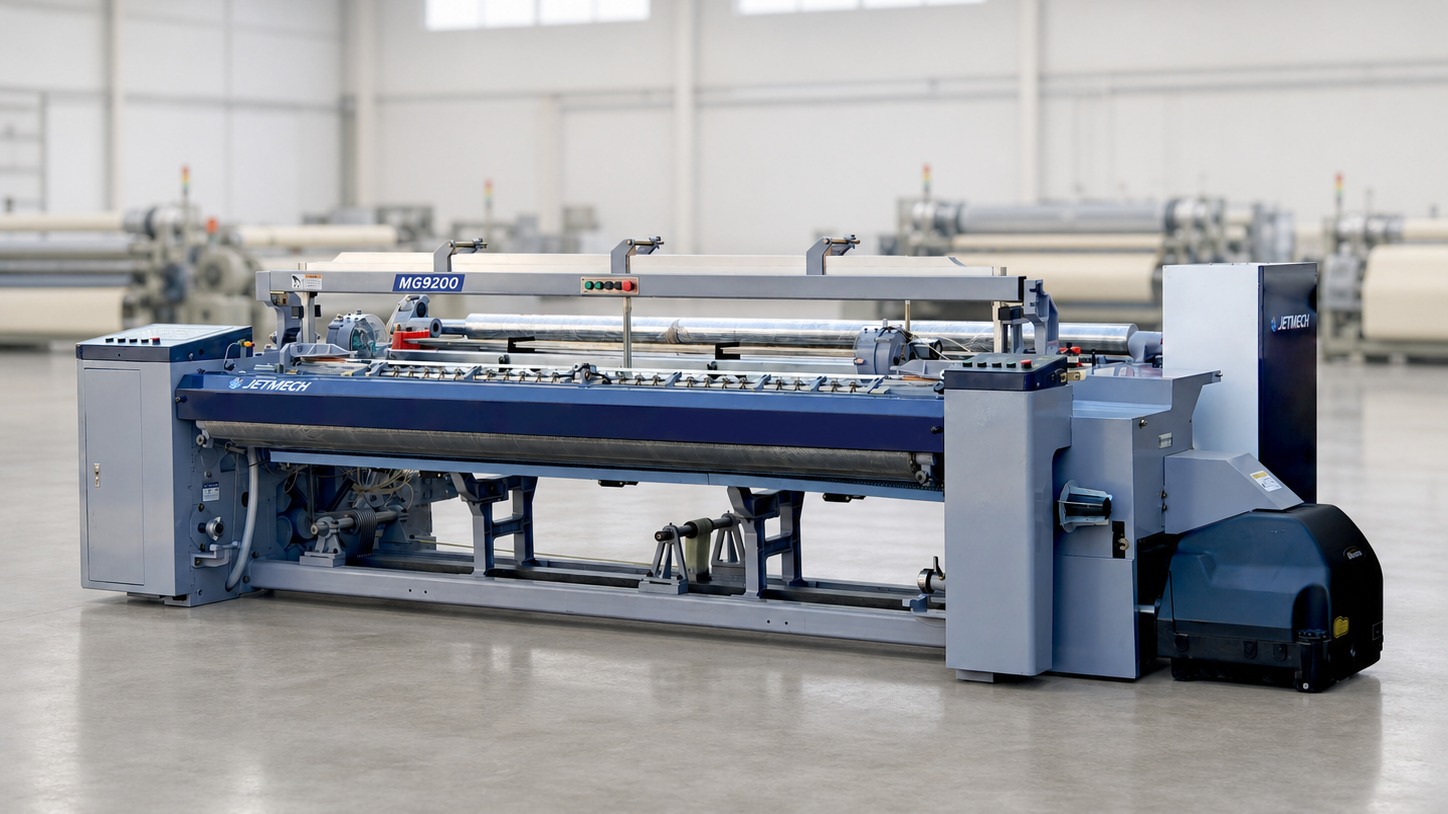
The complete cycle links yarn preparation, shedding, weft measurement, air insertion, detection, beat-up, warp let-off and fabric take-up. Understanding these relationships helps the weaving team evaluate the machine as one coordinated production system.
WEAVING TEAM QUESTIONS
Common checks before configuration
What should the weaving team check first?
The shedding mechanism separates the warp sheets before insertion. A feeder or accumulator prepares the required weft length, the main nozzle starts the yarn, relay nozzles support it across the profiled reed, and the detector confirms arrival. The reed then beats the pick to the cloth fell while let-off and take-up maintain warp delivery and pick density.
Can the same settings or configuration be used for every fabric?
No. Air-jet weaving is a coordinated process. Yarn behavior, fabric construction, reed width, shedding system, air supply and production target can change the correct configuration and process window. Use verified project data and controlled trials instead of copying fixed values.
WEAVING SEQUENCE
One revolution, several coordinated actions
The shedding mechanism separates the warp sheets before insertion. A feeder or accumulator prepares the required weft length, the main nozzle starts the yarn, relay nozzles support it across the profiled reed, and the detector confirms arrival. The reed then beats the pick to the cloth fell while let-off and take-up maintain warp delivery and pick density.
- Shedding creates a clear passage for the pick
- The feeder, stopper and nozzles control release and flight
- Detection confirms that the pick reaches the receiving side
- Beat-up, let-off and take-up convert each pick into stable cloth
SYSTEM COORDINATION
The timing window is shared by the whole loom
Insertion must begin after a usable shed has formed and finish before the shed closes on the yarn. Reed motion, nozzle timing, weft release and detection therefore share one crank-angle window. A change to speed, yarn, width or weave can require the coordinated settings to be reviewed together.
CLOTH FORMATION
Warp tension and pick density complete the process
Electronic or mechanical let-off supplies warp while maintaining the required tension. Take-up advances the cloth at the rate needed for the target pick density. If either motion is unstable, the loom may show density variation, start marks, unclear shedding or repeated stops even when air insertion appears normal.
WEAVING TEAM CHECK
Evaluate the loom as a connected system
A useful machine discussion starts with the fabric construction and follows the yarn through the entire process. This avoids choosing components in isolation and makes the final quotation easier to verify.
Start with the fabric and the complete weaving cycle
Send the fabric construction, warp and weft data, finished width, weave and output target. JETMECH can explain which MG9200 Max systems need to be confirmed for the project.